


 Language


Date:2026-07-02 10:09:38
Access:48
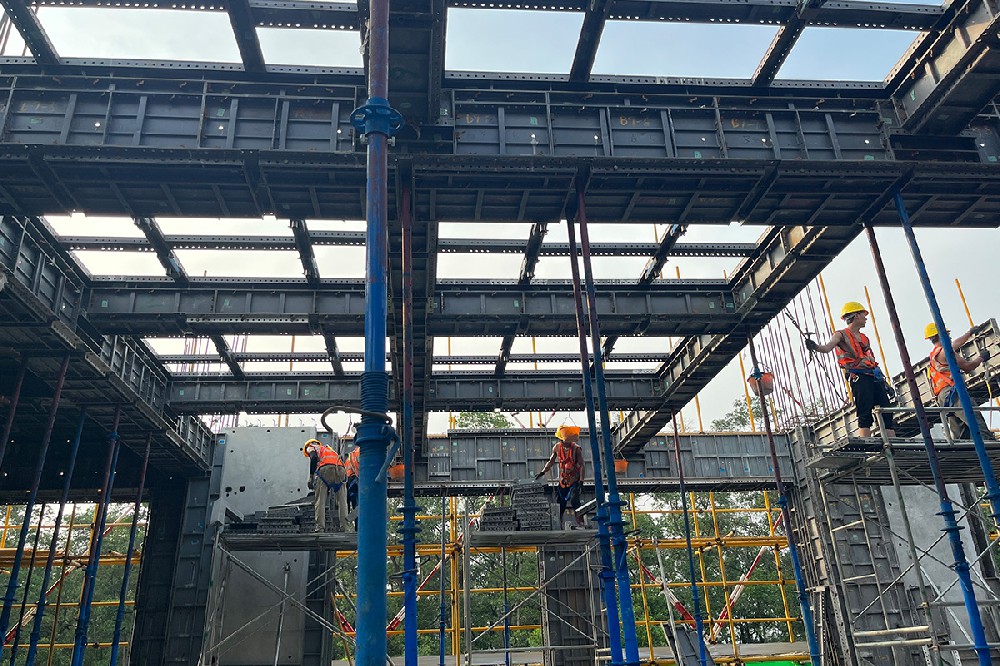
During aluminum formwork construction, although far fewer problems occur than with timber, some typical issues may still arise. Understanding their causes and solutions minimizes schedule delays and quality defects. Based on Archipower’s years of on-site service experience, we summarize common issues and remedies.
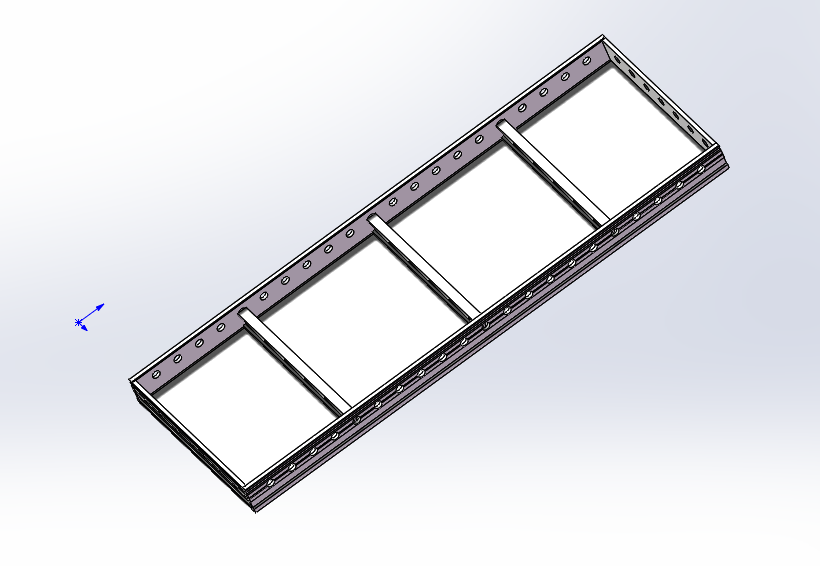
Symptoms: Cement slurry seeping through joints – “skirting” or honeycombing.
Causes:
· Pins not fully driven, wedges loose.
· Panels deformed or edges worn – excessive gaps.
· Missing or aged sealing strips.
· Concrete slump too high – excessive lateral pressure.
Solutions:
· Check each pin during installation; drive wedges tight.
· Inspect edges every 100 uses – replace or weld if worn.
· Replace damaged sealing strips after each cleaning.
· Control slump at 180±20mm.
Symptoms: Concrete residue on panels after stripping – affects next use and wall quality.
Causes:
· Release agent uneven or missed.
· Poor quality release agent (common engine oil sticks).
· Panels not cleaned – old concrete residue.
· Stripped too early – insufficient concrete strength.
Solutions:
· Use dedicated aluminum release agent (oily emulsion or water-based); apply evenly.
· Clean panels with scraper or wire brush after each strip.
· Strip side forms at 12–36 hours, bottom forms at 72+ hours (adjust based on temperature and strength report).
Symptoms: Panel bulging, frame bending, misaligned holes.
Causes:
· Prop spacing too wide or insufficient support rigidity.
· Pouring rate too fast – lateral pressure exceeds design.
· Early stripping of bottom forms – slab weight bends panels.
· Violent stripping with pry bars.
Solutions:
· Follow design prop spacing (wall backing bars ≤600mm, slab props ≤1200mm).
· Control pouring rate – 2–3 lifts per wall/column height.
· Strip based on cylinder strength reports – never early.
· Train workers on correct stripping (remove connectors first, tap from one side).
Symptoms: Opening or box position deviates from drawings – requires chasing later.
Causes:
· Opening molds not securely fixed – shifted during pour.
· Detailed design omitted embedment positioning.
Solutions:
· Weld or wire-tie embedments/opening molds to adjacent panels.
· Archipower‘s detailed design includes all embedment positions – factory-located holes.
Symptoms: Sand streaks, air bubbles, color variation.
Causes:
· Excess release agent pooling – oil marks.
· Inadequate or excessive vibration.
· Debris on panel surface.
Solutions:
· Apply release agent thinly and evenly – no runs.
· Vibrate in layers ≤500mm thick – fast insertion, slow withdrawal.
· Blow off panel surface with compressed air before pouring.
We provide with every shipment:
· A complete installation and troubleshooting guide.
· Consumables including dedicated release agent and sealing strips.
 No.18, North Park Mid Rd,Shishan Town,Nanhai District,Foshan City, Guangdong Province,China
 +86 757 8996 1226
 +86 139 2863 3856
+86 139 2482 7006